A shearing blade is bought once and paid for on every leaf you cut. Get the blade, clearance or press wrong, and you pay three times: in blade cost, in burrs, and in the deburring that follows.
A cheaper blade is not a cheaper cut.
The cost nobody budgets for: deburring
A burr at the sheared end is a notch where a fatigue crack can start, so it has to come off. That means a separate deburring step: people, machines and handling that add nothing to the spring.
Most of that burr is made at the shear: by the wrong clearance, a worn or chipped edge, or blades that move apart under load. Get the shearing right, and the burr stays small and the deburring shrinks with it.
What decides blade life and edge quality
- Clearance set to the thickness: too tight, and the edge is overloaded and chips; too wide, and the steel tears and bends, leaving a burr. Cutting several thicknesses needs clearance that can be adjusted, and held.
- Tooling design: how the blade is held, supported and located decides whether the edge sees a clean cut or a bending load.
- Guides: worn or loose guides let the blades wander under load, so the clearance you set is not the clearance you cut with.
- The press: a stiff frame holds the blades aligned through the cut; a frame that opens under load does not.
- The cut itself: a flat that lifts side-loads the edge, and impact or overload chips it.
- Blade steel and heat treatment: shearing is a shock duty. Too hard, and the edge chips; too soft, and it wears.
- An edge run too long: more load, a bigger burr, and more steel off at regrinding.
How R-Tech shearing gets it right
- Adjustable blade clearance, set to the thickness you cut.
- Tooling and guides designed together with the machine.
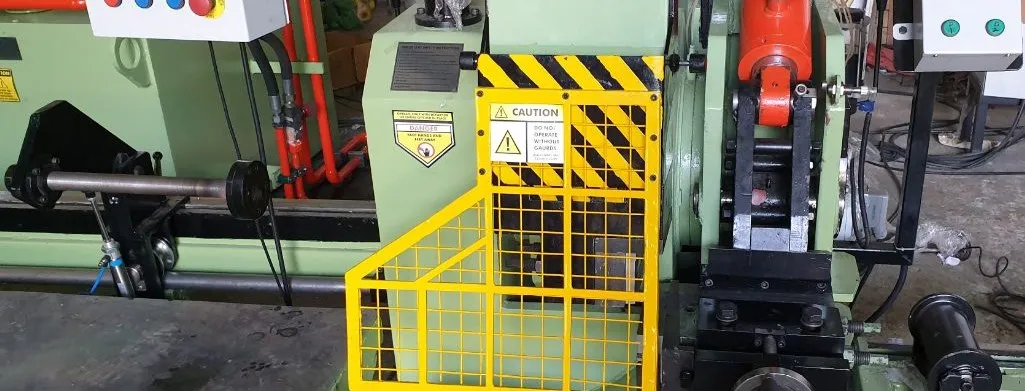
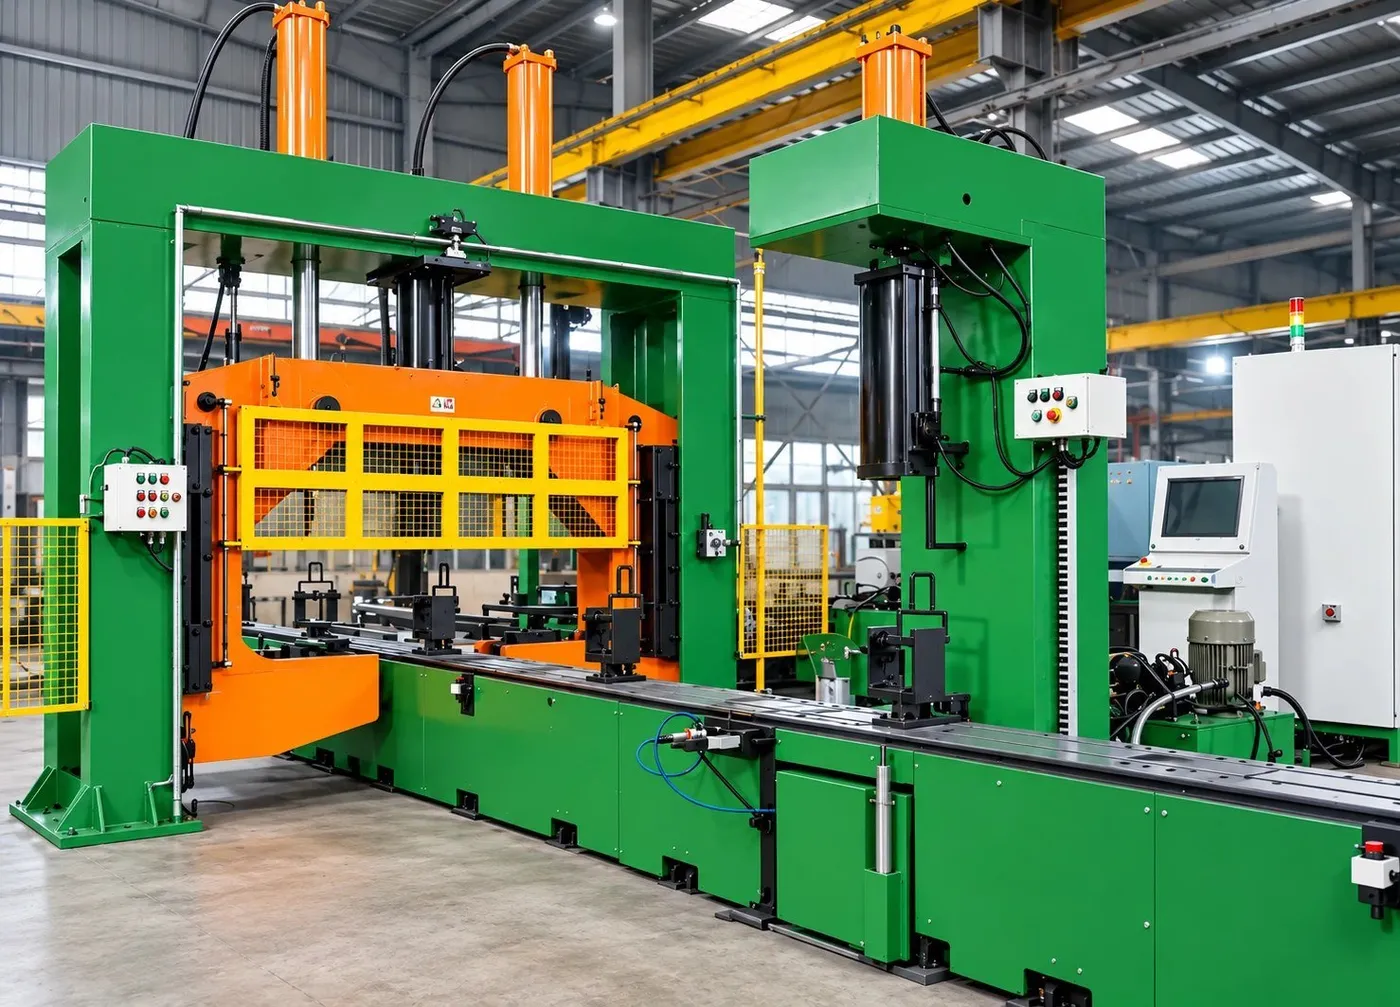
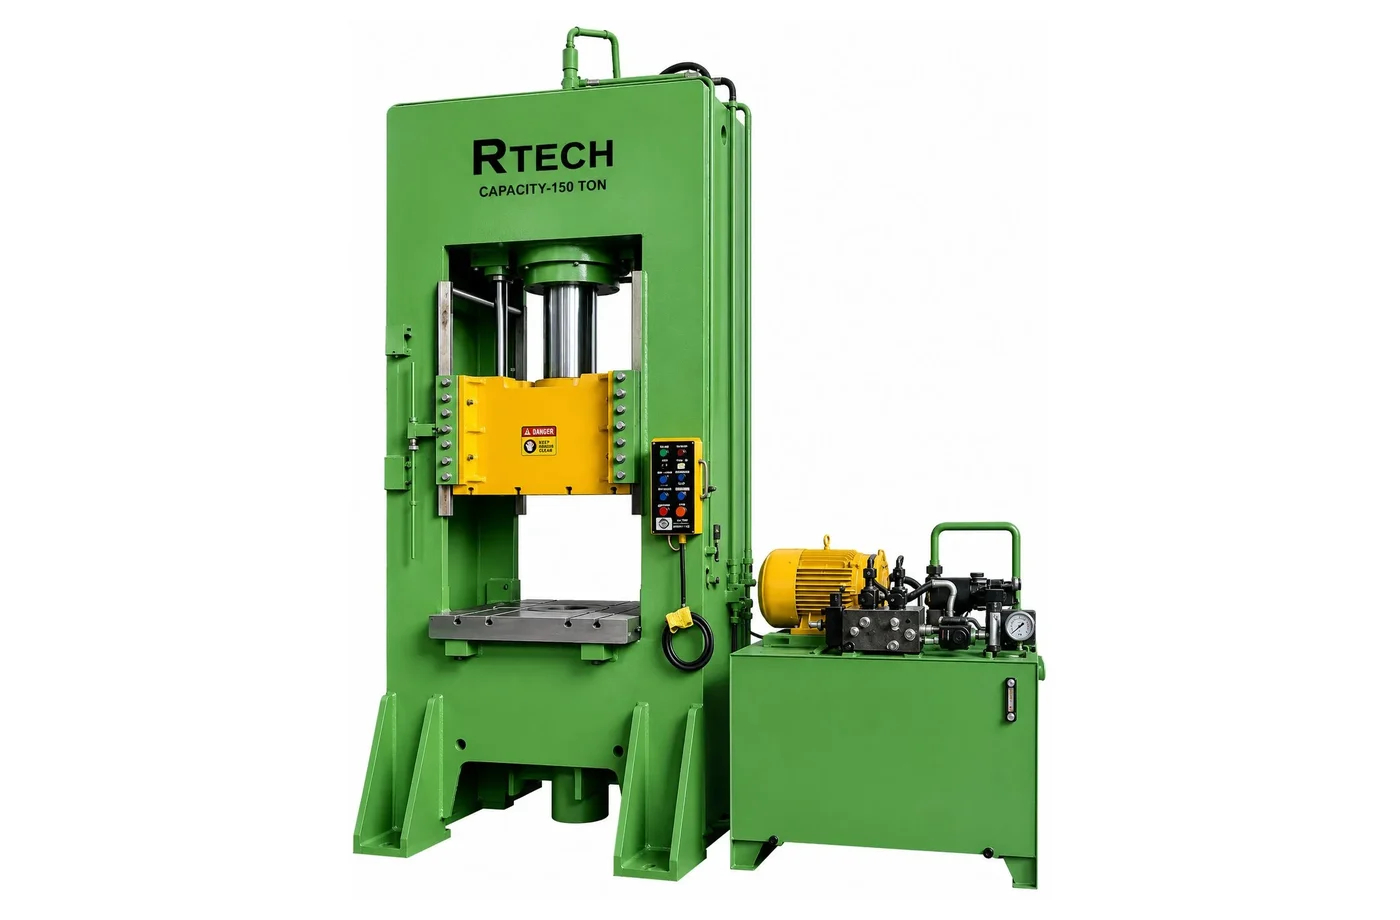
- A closed-frame hydraulic press that keeps the blades aligned, with a controlled cut and force limited by the hydraulic pressure.
- Hydraulic clamping, so the flat cannot lift and the edge cuts square.
- Special proprietary tool steels, with heat treatment chosen for the duty.
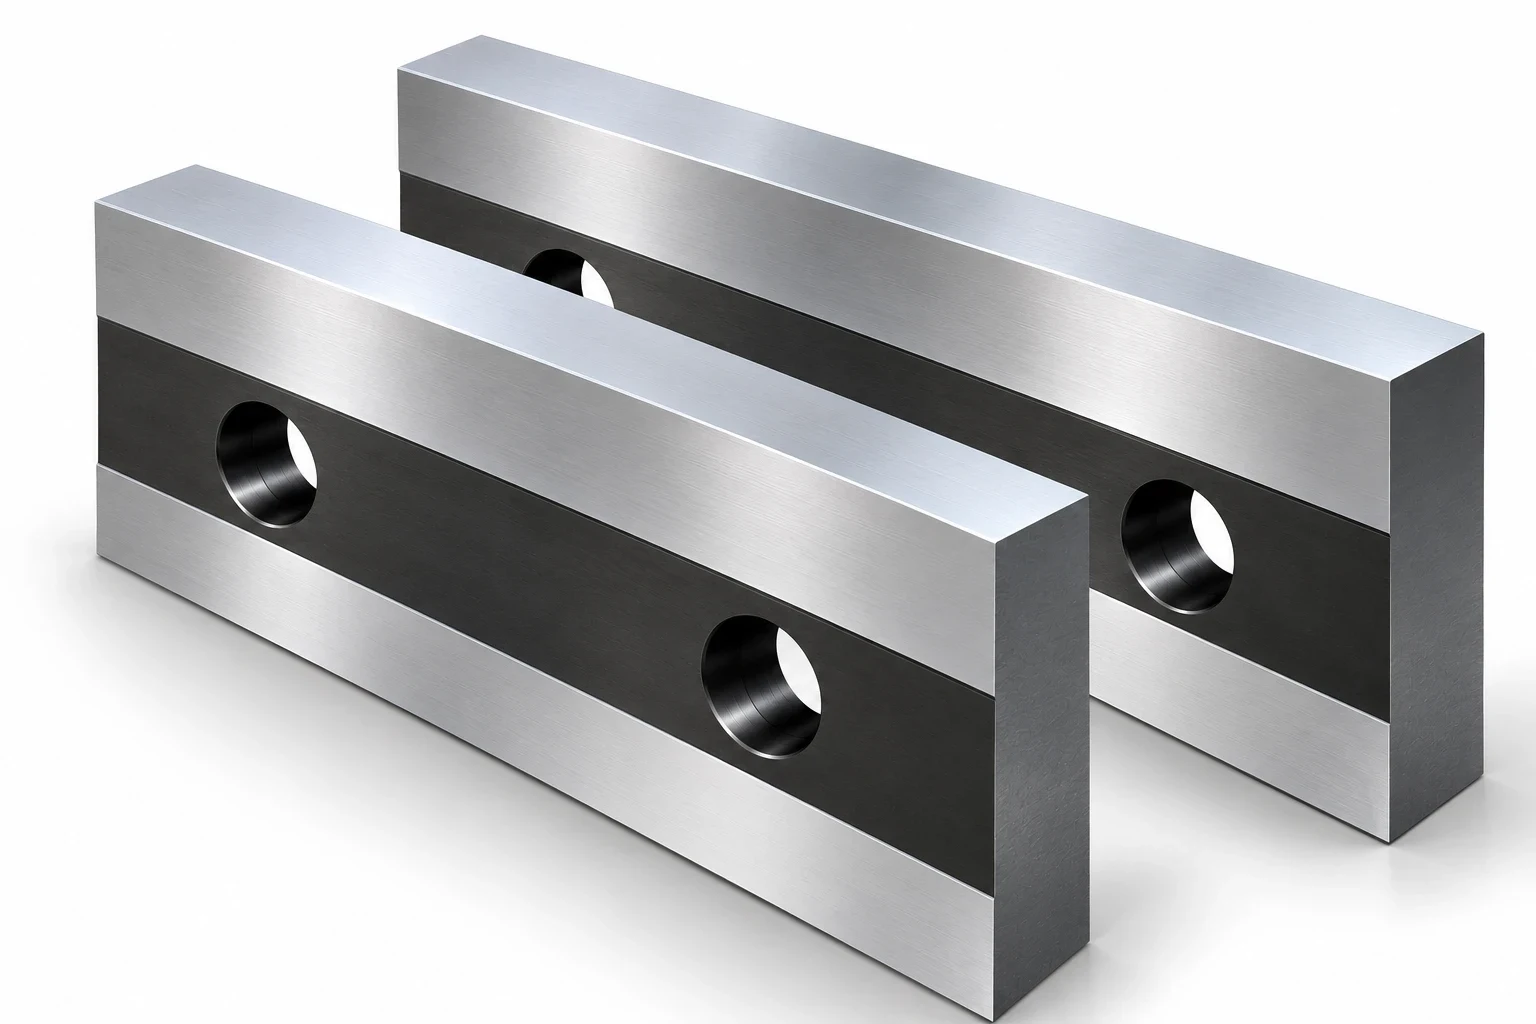
- Four cutting edges per blade, and up to eight in some tooling designs, against two on a conventional blade.
The real saving is in the line
Blade cost per leaf falls when each edge cuts more leaves before regrinding and each blade gives more edges. Add the deburring you no longer need, and fewer blade changes and stops, and the saving shows in the line, not on the blade invoice.
Not just a blade: the complete shearing tooling
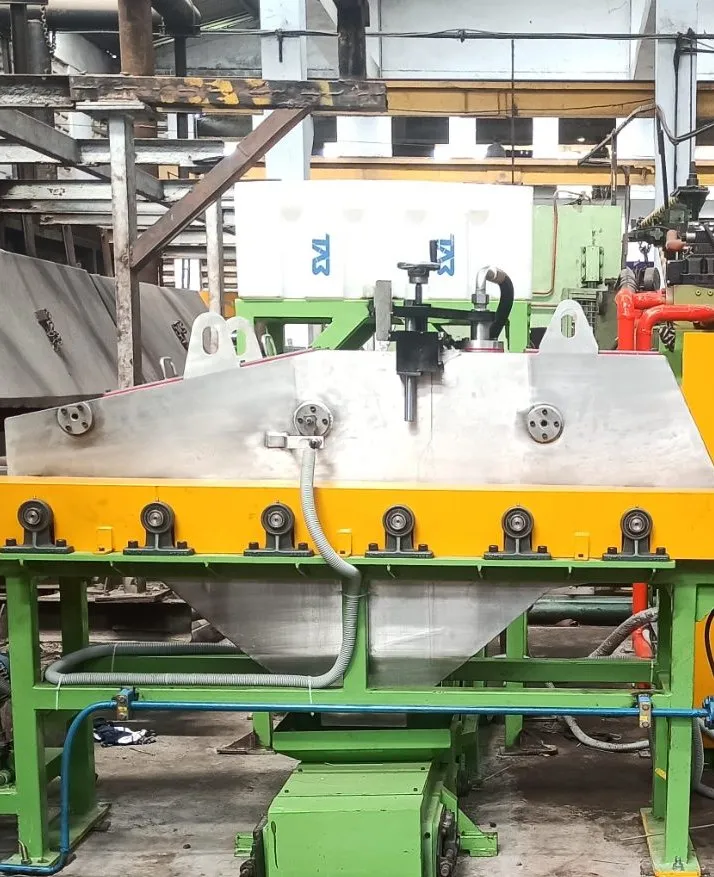
A blade on its own cannot hold its clearance, stop the flat lifting or keep itself aligned. R-Tech supplies the complete shearing tooling: blades, hydraulic clamping, adjustable clearance and a hydraulic press built for the process, up to the complete SPVC shearing cell. Blades and tooling are also available on their own.
Count the cost per leaf, not the price per blade.
Contact us to review your shearing and your blade cost per leaf, and for a quote. Send your blade drawing, the shear you run, your section range and material grade, how many leaves you cut per edge today, and whether your leaves are deburred after shearing.
Images for pictorial purpose only; actual machine may vary.